What Is a Coffee Color Sorting Machine and How Does It Work?
What Is a Coffee Color Sorting Machine?
For coffee processing plants and export factories, maintaining consistent quality is the biggest challenge in post-harvest production. A coffee color sorting machine (also known as an optical sorter) is the key technology used to automate quality control and ensure your product meets premium standards.
Here is a simple explanation of what a coffee color sorter is, how it operates, and why it is essential for modern coffee exporters.
What is a Coffee Color Sorting Machine?
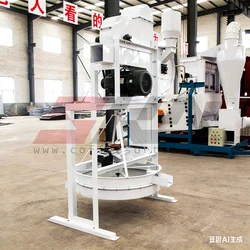
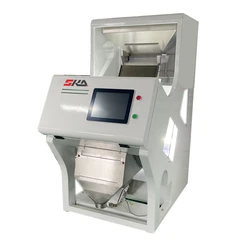
A coffee color sorting machine is an advanced industrial optical sorting system designed to separate defective coffee beans and foreign materials from clean green coffee.
Instead of relying on slow manual labor, the machine uses high-speed optical sensors, cameras, and air ejectors to scan and sort coffee beans in real time based on color, shape, and texture differences.
How a Coffee Color Sorter Works
The sorting process happens in milliseconds through a highly efficient four-step system:
Feeding and Distribution Unsorted green coffee beans are loaded into the hopper at the top. Vibratory feeders distribute the beans evenly across inclined chutes or belts, ensuring they slide down in a single, consistent layer.
Optical Scanning As the coffee beans free-fall from the end of the chutes, high-resolution cameras and optical sensors scan each bean from multiple angles. Modern machines use advanced full-color CCD cameras or infrared technology to detect even the slightest discoloration.
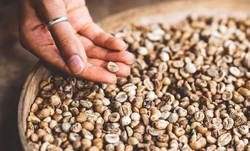
Defect Analysis and Recognition The machine's processing system analyzes the camera images in real time. It compares each bean to your preset sorting standards, instantly identifying defects like black beans, sour beans, moldy beans, and foreign materials (such as stones, glass, or sticks).
Precision Ejection Once a defect is detected, the system signals the pneumatic ejectors. High-speed air valves shoot a precise puff of compressed air to knock the bad bean out of the product stream and into the reject chute, while the clean, high-quality beans continue falling safely into the accepted container.
Key Applications in the Coffee Industry
Automated color sorting is a standard setup in several areas of the industry:
Coffee Export Factories: Used to clean bulk green coffee to meet strict international defect tolerances before shipping container loading.
Dry Milling Processing Plants: Placed after hulling and size grading to perform the final, highest-precision quality check.
Specialty Coffee Production: Ensuring micro-lots are completely free of sour, immature, or broken beans to protect the cup profile and command premium prices.
Why Your Factory Needs an Optical Sorter
Relying on manual hand-sorting is no longer viable for commercial volumes. It is too slow, expensive, and inconsistent due to human fatigue.
Integrating a coffee color sorting machine into your production line delivers consistent sorting accuracy 24/7, dramatically reduces labor costs, and guarantees you deliver export-grade coffee that commands top prices in the global market.
Get a Custom Coffee Sorting Solution
Are you looking to improve your coffee quality or upgrade your dry mill capacity? Contact our technical team today to discuss your daily throughput and find the right optical sorting configuration for your business.